Product Parameters:
1. Machine Overview
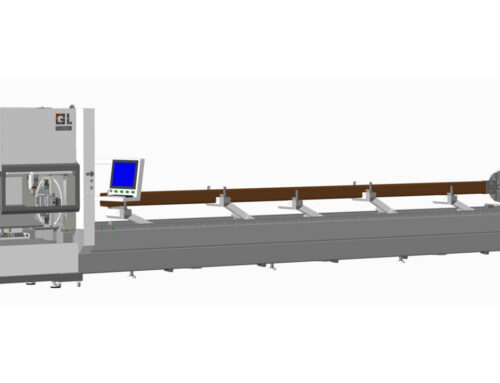
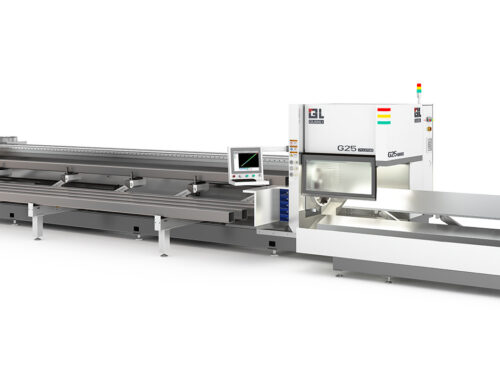
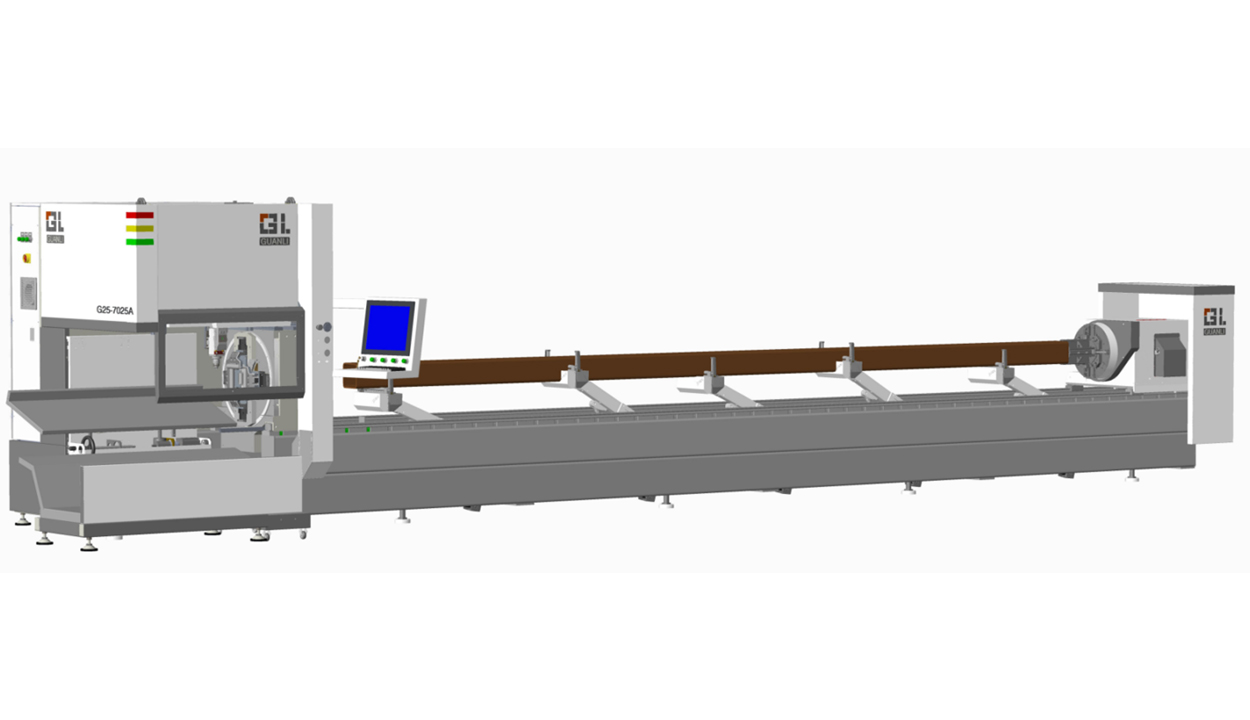
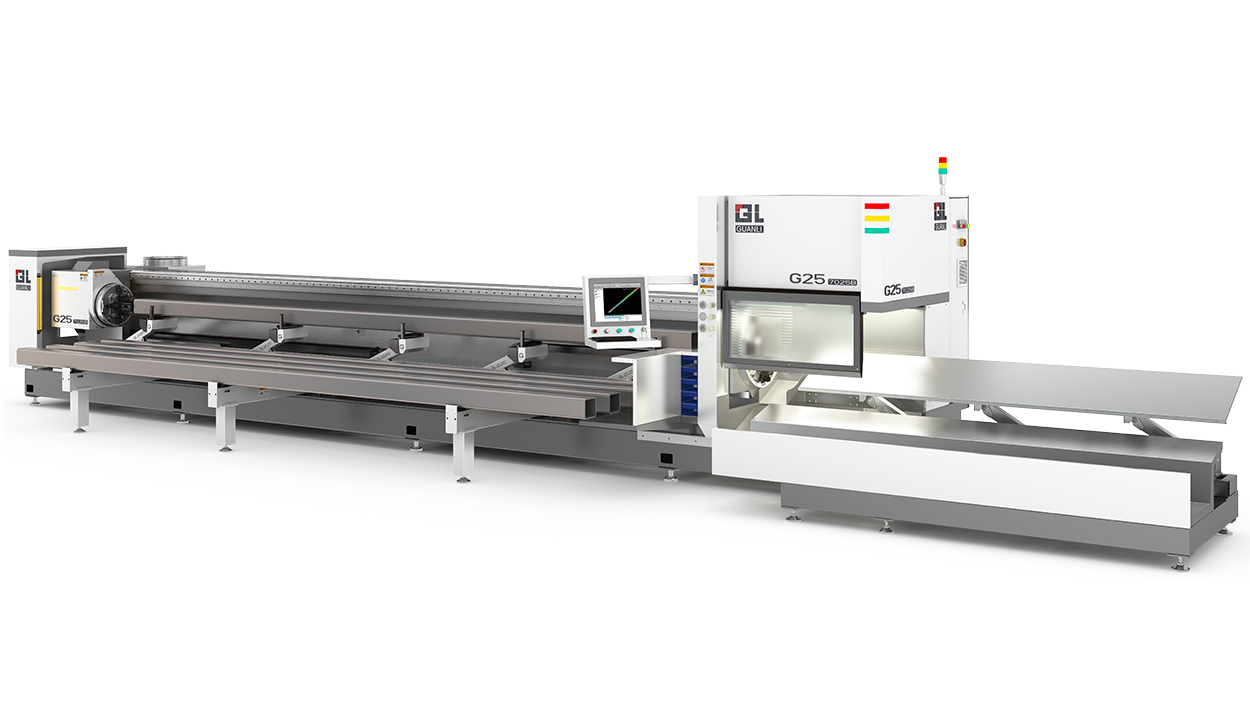
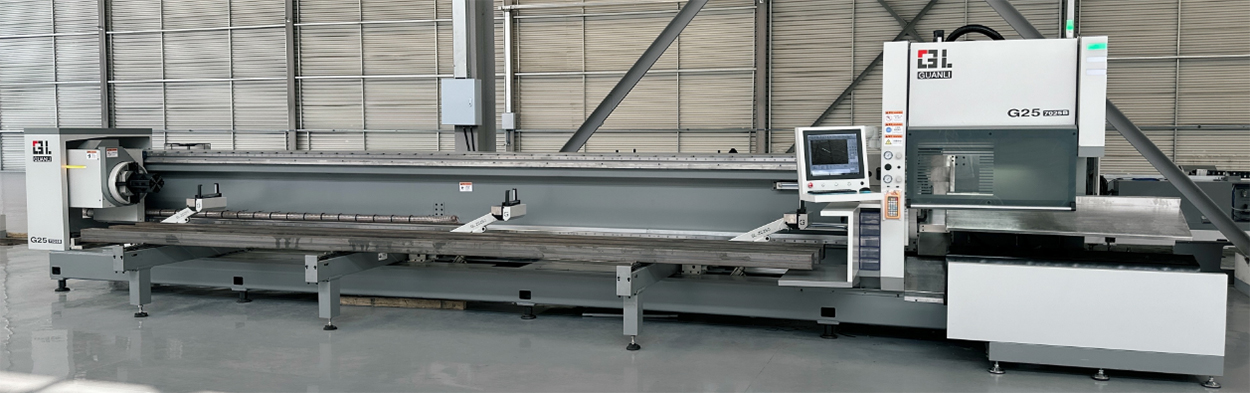
Identical machine structure to the G25-7025B-3000W — split-type bed, 120 RPM / 1.2G chuck, Ø15–250 mm round/square/oval/special-profile range, 20–45 mm short remnant — but equipped with a 6000 W fiber source. The step from 3000 W to 6000 W roughly doubles the usable thickness envelope on stainless steel and aluminum and adds high-speed cutting on thin walls, which is why this version is the default choice for structural fabricators cutting thicker-walled tube.
2. Key Advantages
- 6000 W source: up to 30 mm carbon steel, 25 mm stainless steel, 25 mm aluminum alloy.
- Tube range Ø15–250 mm — round, square, oval and special profiles.
- Chuck rated at 120 RPM / 1.2G with 20–22 s semi-automatic loading.
- 20–45 mm short tail remnant for maximum yield per bar.
- Split-type welded bed annealed at 600 °C for long-term stability.
- Running cost approx. CNY 20–25 per hour.
3. Welded Machine Bed & Structure
The split-type construction (main machine bed + unloading bed) is welded from steel plates and tubular sections, stress-relief annealed at 600 °C with a 4.5-hour hold and furnace cooling, then rough and precision machined. A stiffer, stress-free bed matters more at 6000 W, where higher cutting forces and faster accelerations would otherwise expose any residual stress as inaccuracy.
4. Automatic Loading System
The semi-automatic loading system runs a 20–22 s cycle: the centering clamping jaw positions the raw tube, the rear clamp grips the profile and feeds it forward into the front chuck. Cut parts drop onto the separate unloading bed, keeping heavy thick-wall tubes flowing without manual handling at the cutting zone.
5. Cutting Performance
Reference cutting data for the 6000 W source (carbon steel Q235 with oxygen; dual ranges on thin material quoted from the factory parameter table):
| Material | Thickness (mm) | Cutting Speed (m/min) | Assist Gas |
|---|---|---|---|
| Carbon steel Q235 | 1 | 8.0–12 / 35–50 | Oxygen |
| Carbon steel Q235 | 3 | 3.5–5.0 / 15–20 | Oxygen |
| Carbon steel Q235 | 6 | 2.6–3.2 | Oxygen |
| Carbon steel Q235 | 10 | 2.0–2.6 | Oxygen |
| Carbon steel Q235 | 20 | 0.7–0.9 | Oxygen |
| Carbon steel Q235 | 30 | 0.15–0.2 | Oxygen |
| Stainless steel 304 | 1 | 35–60 | Nitrogen |
| Stainless steel 304 | 3 | 15–19 | Nitrogen |
| Stainless steel 304 | 6 | 5.0–8.0 | Nitrogen |
| Stainless steel 304 | 10 | 2.3–3.0 | Nitrogen |
| Stainless steel 304 | 20 | 0.2–0.3 | Nitrogen |
| Stainless steel 304 | 25 | 0.15–0.2 | Nitrogen |
| Aluminum alloy | 1 | 35–60 | Nitrogen |
| Aluminum alloy | 3 | 12–18 | Nitrogen |
| Aluminum alloy | 6 | 4–5.5 | Nitrogen |
| Aluminum alloy | 10 | 1.5–2.3 | Nitrogen |
| Aluminum alloy | 16 | 0.5–0.8 | Nitrogen |
| Aluminum alloy | 25 | 0.12–0.2 | Nitrogen |
| Brass | 1 | 30–60 | Nitrogen |
| Brass | 3 | 15–18 | Nitrogen |
| Brass | 6 | 4.2–5.5 | Nitrogen |
| Brass | 10 | 1–1.6 | Nitrogen |
| Brass | 16 | 0.5–0.7 | Nitrogen |
| Copper | 1 | 30–60 | Oxygen |
| Copper | 3 | 12–15 | Oxygen |
| Copper | 6 | 2.5–4.5 | Oxygen |
| Copper | 10 | 0.7–1.2 | Oxygen |
6. Power, Cooling & Gas Requirements
Gas supply for the 6000 W source: nitrogen ≥ 2.0 MPa; air ≥ 1.3 MPa (≥ 2.5 m³/min); oxygen ≥ 1.0 MPa.
| Item | Requirement |
|---|---|
| Power supply | Three-phase five-wire 380–400 VAC, 50 Hz; recommended capacity ≥ 60 kVA, voltage stability ± 2%, grounding resistance ≤ 3 Ω |
| Cooling water | 40 L distilled / deionized water, conductivity < 10 µS/cm |
| Assist gas | Oxygen purity ≥ 99.6%; nitrogen purity ≥ 99.99%; supply pressures: N₂ ≥ 2.0 MPa, air ≥ 1.3 MPa (≥ 2.5 m³/min), O₂ ≥ 1.0 MPa |