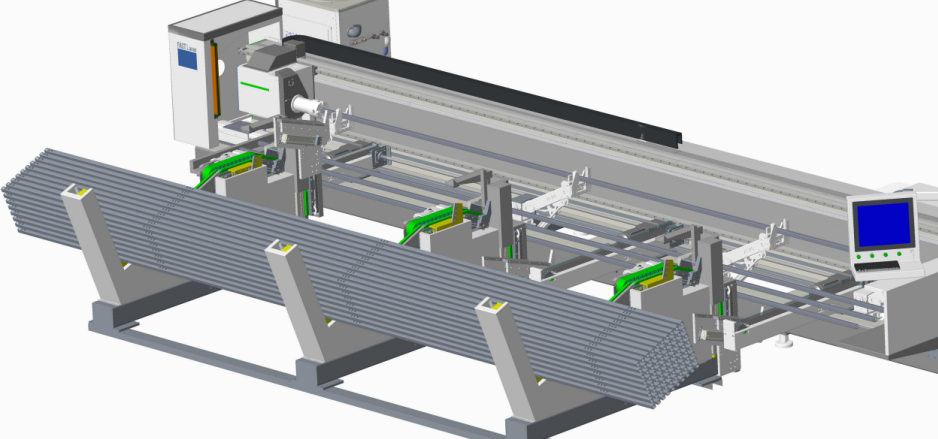
Product Parameters:
1. Machine Overview
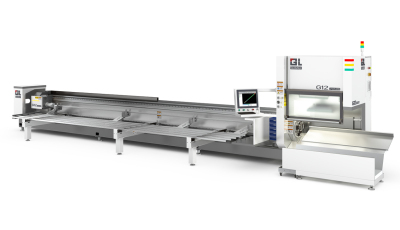
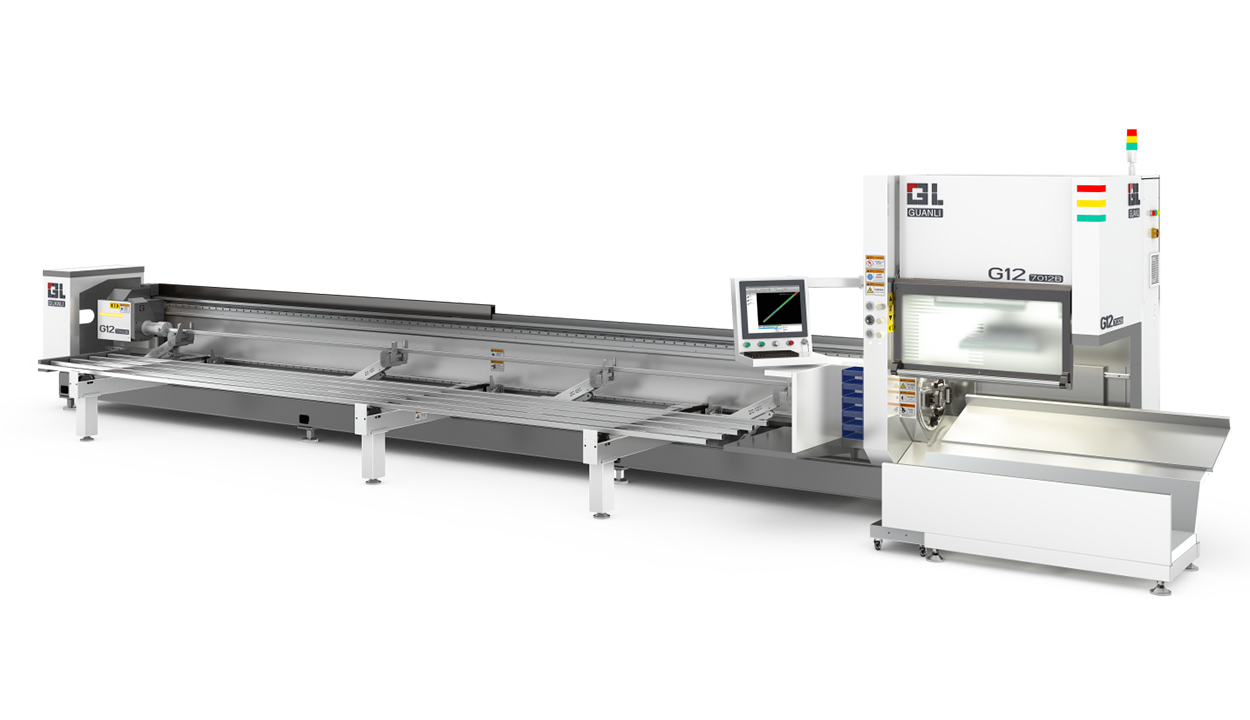
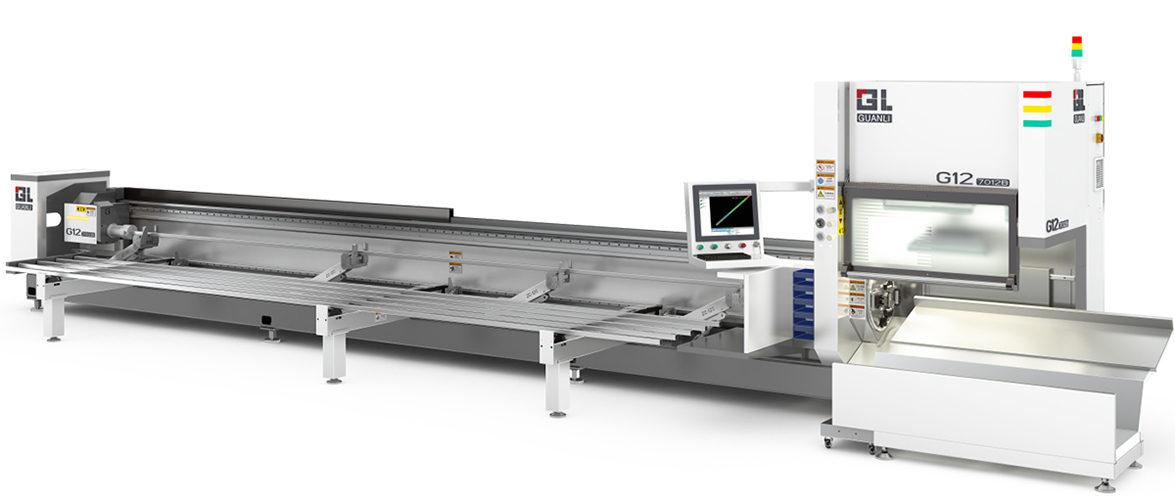
The G12-7012B-3000W Automatic pairs the G12 small-platform structure — a side-mounted (cantilever) layout with welded, stress-relieved bed — with an automatic loading machine for unmanned tube feeding. It clamps round, square, oval and special-profile tubes from Ø10 mm to Ø120 mm in a single chucking, and leaves only a 20–45 mm end remnant thanks to chuck avoidance, so more of every 6 m stock bar becomes sellable parts.
2. Key Advantages
- High-speed chuck rated at 160 RPM / 1.5G for fast rotary cutting.
- Tube range Ø10–120 mm — round, square, oval and special profiles in one machine.
- 18–19 s loading cycle keeps spindle idle time to a minimum.
- Ultra-short 20–45 mm tail remnant (chuck avoidance) reduces material waste.
- Running cost of approx. CNY 13–15 per hour — the most economical platform in the Gelian tube line-up.
- Welded bed annealed at 600 °C for long-term accuracy retention.
3. Welded Machine Bed & Structure
The bed is fabricated from welded steel plates and tubular sections, then stress-relief annealed at 600 °C (held and furnace-cooled) before rough and finish machining. This eliminates internal welding stress so the bed keeps its geometry over years of shifts. The side-mounted structure leaves the loading side open, which is what makes the automatic loading machine and convenient unloading possible on this variant.
4. Automatic Loading System
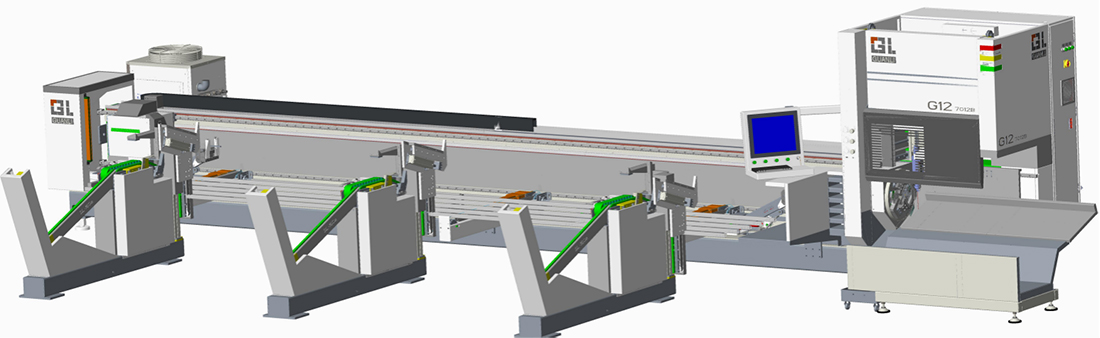
On the G12 platform the loading cycle is quoted at 18–19 s. This automatic variant integrates the automatic loading machine with the side-mounted structure, so raw tubes are fed, centered and clamped without an operator lifting every bar — ideal for longer production runs on smaller-diameter tube and profile work.
5. Cutting Performance
Reference cutting data for the 3000 W source (carbon steel with oxygen/air assist, piercing 0.1–0.8 s):
| Material | Thickness (mm) | Cutting Speed (m/min) | Assist Gas |
|---|---|---|---|
| Carbon steel | 1 | 7–10 / 20–25 | Oxygen / air |
| Carbon steel | 2 | 5–7.5 / 13–17 | Oxygen / air |
| Carbon steel | 4 | 3.5–4.5 | Oxygen / air |
| Carbon steel | 8 | 1.6–2.3 | Oxygen / air |
| Carbon steel | 12 | 0.9–1.2 | Oxygen / air |
| Stainless steel | 1 | 20–25 | Nitrogen |
| Stainless steel | 2 | 12–15 | Nitrogen |
| Stainless steel | 4 | 3.5–4.5 | Nitrogen |
| Stainless steel | 6 | 1.3–1.8 | Nitrogen |
| Stainless steel | 8 | 0.8–1 | Nitrogen |
| Aluminum alloy | 1 | 20–25 | Nitrogen |
| Aluminum alloy | 2 | 13–17 | Nitrogen |
| Aluminum alloy | 4 | 3.5–4.5 | Nitrogen |
| Aluminum alloy | 6 | 1.3–1.8 | Nitrogen |
| Brass | 1 | 22–26 | Nitrogen |
| Brass | 2 | 10–15 | Nitrogen |
| Brass | 4 | 2.5–3.5 | Nitrogen |
| Brass | 6 | 1–1.5 | Nitrogen |
| Copper | 1 | 20–25 | Oxygen |
| Copper | 2 | 9–12 | Oxygen |
| Copper | 3 | 3.5–5.5 | Oxygen |
| Copper | 4 | 2.2–2.5 | Oxygen |
6. Power, Cooling & Gas Requirements
| Item | Requirement |
|---|---|
| Power supply | Three-phase five-wire 380–400 VAC, 50 Hz; recommended capacity ≥ 60 kVA, voltage stability ± 2%, grounding resistance ≤ 3 Ω |
| Cooling water | 40 L distilled / deionized water, conductivity < 10 µS/cm |
| Assist gas | Oxygen purity ≥ 99.6%; nitrogen purity ≥ 99.99% |