Product Parameters:
1. Machine Overview
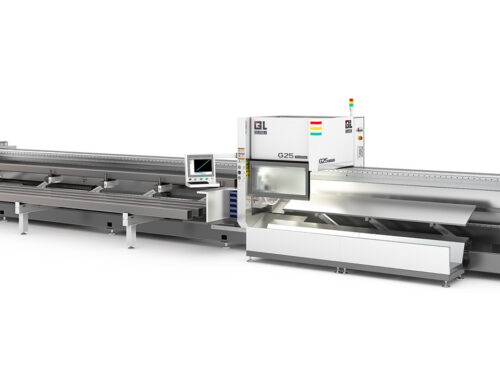
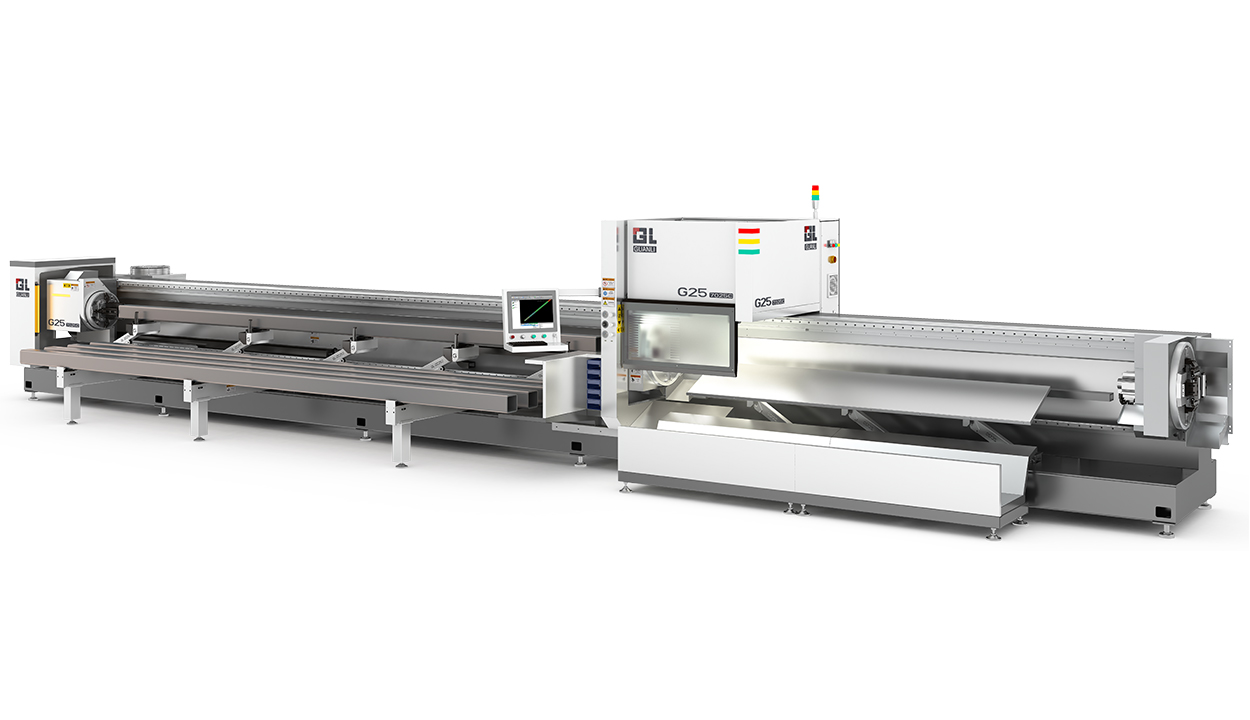
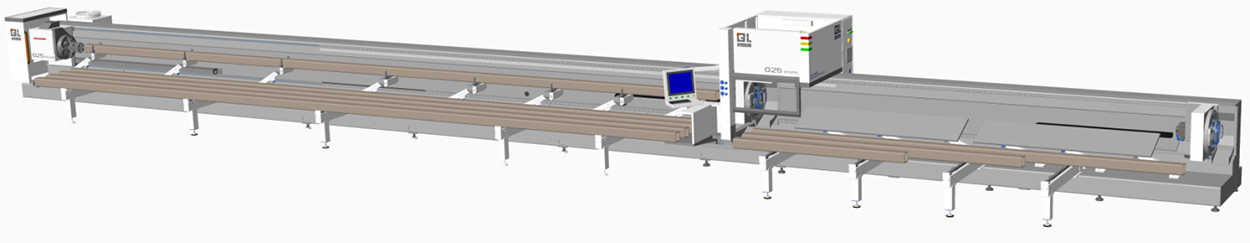
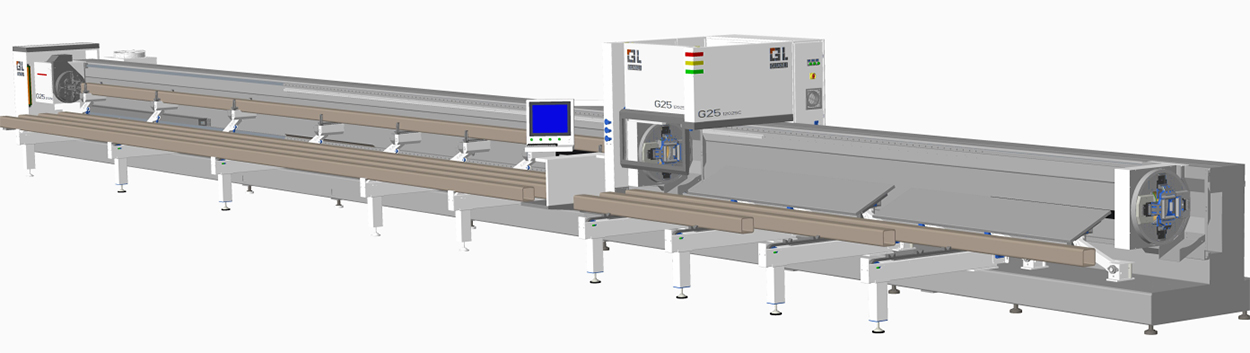
The GT25-12025C-6000W extends the GT25 family (G25B platform parameters) to the longer 12025-class platform, here with a 4 m unloading bed. Core figures match the series: 120 RPM / 1.2 G chuck axis, Φ15–250 mm clamping for round, square, oval and special profiles, 20–22 s semi-automatic loading, 20–45 mm tail waste and roughly CNY 20–25/h running cost. The 6,000 W source adds heavy-wall capacity for structural tube work.
2. Key Advantages
- Longer 12025 platform with a 4 m unloading bed — long raw tubes in, long cut parts out, fully supported.
- 6,000 W cutting range — carbon steel to 30 mm, stainless/aluminum to 25 mm, brass to 16 mm, copper to 12 mm.
- 120 RPM / 1.2 G chuck across Φ15–250 mm.
- 20–22 s loading cycle and 20–45 mm tails.
- 600 °C / 4.5 h annealed welded bed, split main + unloading layout.
- ≈ CNY 20–25/h running cost.
3. Welded Machine Bed & Structure
The bed is welded from steel plate and tube, annealed at 600 °C with a 4.5-hour hold and furnace cooling to eliminate stress, then rough- and finish-machined. On the 12025C the split design pairs the long main cutting bed with the separate 4 m unloading bed; the side-suspended chuck leaves the tube line open for loading and support.
4. Automatic Loading System
Semi-automatic loading takes 20–22 seconds per bar. Cut parts are received on the 4 m unloading bed, keeping discharge separated from the cutting zone so the machine can keep cutting while finished parts are removed.
5. Cutting Performance
With 6,000 W the machine cuts carbon steel (Q235) to 30 mm, stainless steel (304) and aluminum to 25 mm, brass to 16 mm and copper to 12 mm; 1 mm stainless and aluminum run at 35–60 m/min. Representative cutting speeds:
| Material | Thickness (mm) | Cutting Speed (m/min) | Assist Gas |
|---|---|---|---|
| Carbon steel Q235 | 1 | 8.0–12 / 35–50 | Oxygen |
| Carbon steel Q235 | 3 | 3.5–5.0 / 15–20 | Oxygen |
| Carbon steel Q235 | 6 | 2.6–3.2 | Oxygen |
| Carbon steel Q235 | 10 | 2.0–2.6 | Oxygen |
| Carbon steel Q235 | 20 | 0.7–0.9 | Oxygen |
| Carbon steel Q235 | 30 | 0.15–0.2 | Oxygen |
| Stainless steel 304 | 1 | 35–60 | Nitrogen |
| Stainless steel 304 | 3 | 15–19 | Nitrogen |
| Stainless steel 304 | 6 | 5.0–8.0 | Nitrogen |
| Stainless steel 304 | 10 | 2.3–3.0 | Nitrogen |
| Stainless steel 304 | 20 | 0.2–0.3 | Nitrogen |
| Stainless steel 304 | 25 | 0.15–0.2 | Nitrogen |
| Aluminum alloy | 1 | 35–60 | Nitrogen |
| Aluminum alloy | 3 | 12–18 | Nitrogen |
| Aluminum alloy | 6 | 4–5.5 | Nitrogen |
| Aluminum alloy | 10 | 1.5–2.3 | Nitrogen |
| Aluminum alloy | 16 | 0.5–0.8 | Nitrogen |
| Aluminum alloy | 25 | 0.12–0.2 | Nitrogen |
| Brass | 1 | 30–60 | Nitrogen |
| Brass | 3 | 15–18 | Nitrogen |
| Brass | 6 | 4.2–5.5 | Nitrogen |
| Brass | 10 | 1–1.6 | Nitrogen |
| Brass | 16 | 0.5–0.7 | Nitrogen |
| Copper | 1 | 30–60 | Oxygen |
| Copper | 3 | 12–15 | Oxygen |
| Copper | 6 | 2.5–4.5 | Oxygen |
| Copper | 10 | 0.7–1.2 | Oxygen |
6. Power, Cooling & Gas Requirements
Gas supply pressures: nitrogen ≥ 2.0 MPa; compressed air ≥ 1.3 MPa with flow ≥ 2.5 m³/min; oxygen ≥ 1.0 MPa.
| Item | Requirement |
|---|---|
| Power supply | Three-phase five-wire 380–400 VAC, 50 Hz; recommended capacity ≥ 60 kVA, voltage stability ± 2%, grounding resistance ≤ 3 Ω |
| Cooling water | 40 L distilled / deionized water, conductivity < 10 µS/cm |
| Assist gas | Oxygen purity ≥ 99.6%; nitrogen purity ≥ 99.99%; supply pressures: N₂ ≥ 2.0 MPa, air ≥ 1.3 MPa (≥ 2.5 m³/min), O₂ ≥ 1.0 MPa |
7. Key component configuration
| No. | Component | Brand | Model / Specification |
|---|---|---|---|
| Key Components | |||
| 1 | Fiber Laser Source | Raycus | 6000W / Domestic first-tier brand |
| 2 | Cutting Head | Guanli / Ospri | Tube-cutting R&D dedicated 6000W / Domestic first-tier brand |
| 3 | Rack and Pinion | YYC | M2-6 grade / Taiwan, China |
| 4 | Reducer | MOTOREDUCER | 110-090 / France |
| 5 | Linear Guide Rail | AIRTAC | CGH35 / Taiwan, China |
| 6 | Motor | Inovance | High-performance motor, 4000rpm bus-type / Domestic first-tier brand |
| 8 | Water Chiller | Hanli / S&A | Domestic first-tier brand |
| 9 | Electrical Control Components | Schneider | France |
| 10 | Pneumatic Components | AIRTAC | Taiwan, China |
| Machining Components | |||
| 11 | Main Machine Bed | Independently developed, Suzhou | 18.5 m / high-temperature annealing |
| 12 | Chuck | Independently developed, Suzhou | QL-250 pneumatic (2-jaw max load 220 kG, 3-jaw max load 300 kG), continuous supply clamping |
| 13 | Auxiliary Loading and Servo Floating Support Rack | Independently developed, Suzhou | 7 supports / load capacity 300 kg |
| 14 | Semi-automatic Loading Device | Independently developed, Suzhou | 3 conveyor units, stores 5 tubes for automatic continuous loading |
| 15 | Unloading Device, Unloading Frame | Independently developed, Suzhou | Servo follow-up unloading flap + unloading conveyor, max 4 m unloading, 40 kg per meter |
| Software System | |||
| 16 | Operating System | Shanghai Bochu | 5000 bus-type system / Shanghai |
| 17 | Nesting Software | Shanghai Bochu | Dedicated 3D tube-cutting software / Shanghai |
| Others | |||
| 18 | Operation Direction | Left-hand machine | Standard |
| 19 | Packaging and Transportation | Standard packaging | Standard |
Note: Industrial power supply: 380V ±5V. Customers should add a voltage stabilizer according to actual site conditions.