Product Parameters:
1. Machine Overview
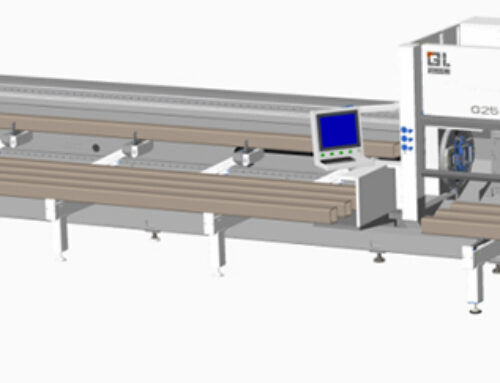
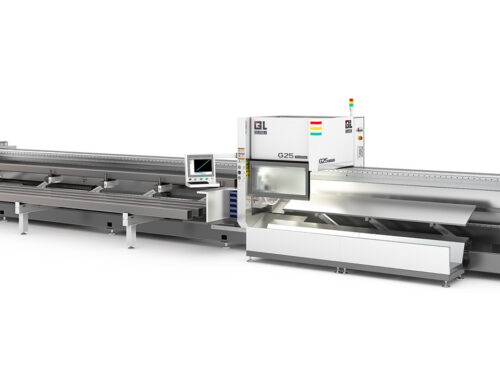
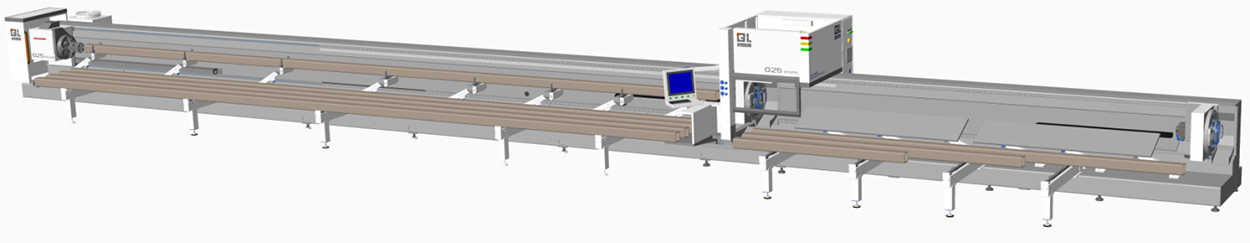
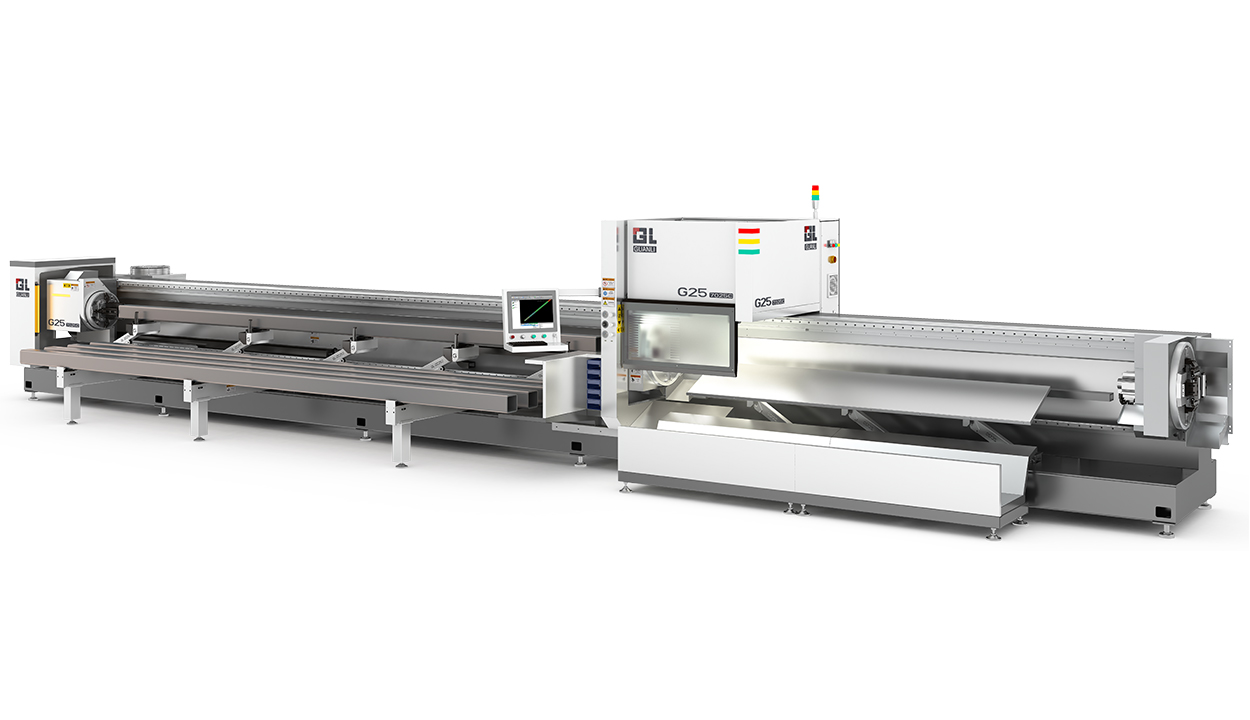
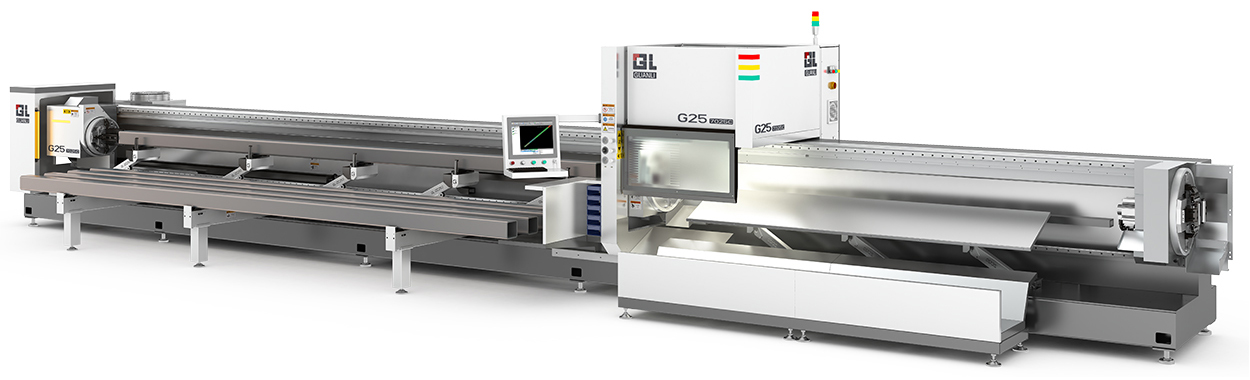
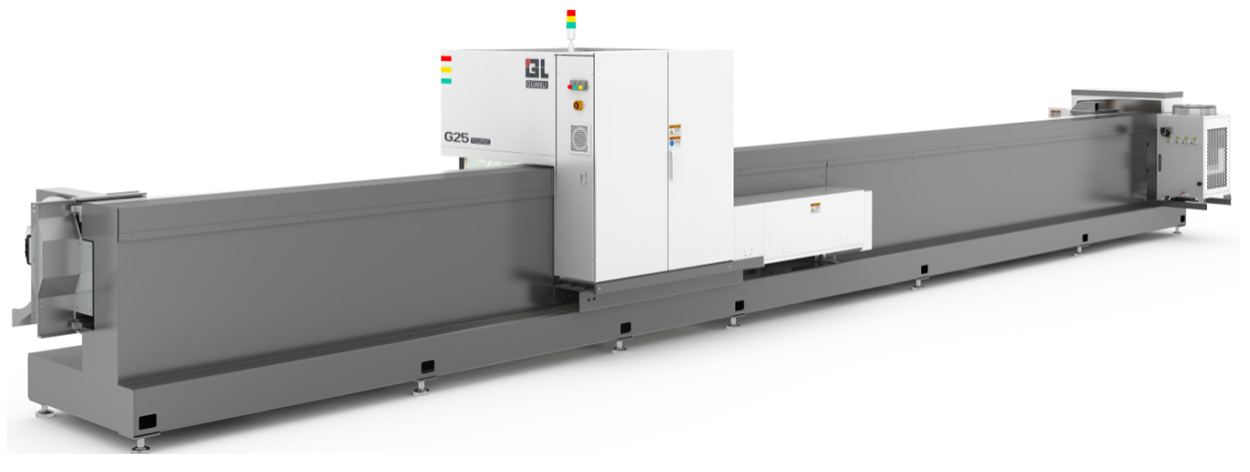
The GT25-7025P-3000W is a 3,000 W GT25-series tube cutting machine on the 7025 platform. Like the whole GT25 line it inherits the G25B parameter set: side-suspended chuck, split welded bed with a separate unloading bed, and support for round, square, oval and special-profile tubes from Φ15 mm to Φ250 mm. Tail waste stays between 20–45 mm and running cost around CNY 20–25/h, suiting it to continuous job-shop work on mixed profiles.
2. Key Advantages
- 120 RPM / 1.2 G rotary axis — fast, responsive chuck for complex contours.
- Φ15–250 mm, four profile families — round, square, oval and special shapes.
- 0.1–0.8 s piercing on carbon steel — short non-cut time between features.
- 20–22 s loading / 20–45 mm tails — fast bar changes with low scrap.
- 600 °C / 4.5 h annealed bed — welded plate-and-tube construction, finish-machined.
- ≈ CNY 20–25/h running cost.
3. Welded Machine Bed & Structure
The bed is welded from steel plate and tube and stress-relieved at 600 °C for 4.5 hours with furnace cooling, then rough-machined and finish-machined for long-term rigidity. The split layout separates the main cutting bed from the unloading bed, and the side-suspended chuck keeps the working line accessible along the whole tube length.
4. Automatic Loading System
The semi-automatic loader feeds bars to the side-suspended chuck in 20–22 seconds per cycle. Finished parts land on the dedicated unloading bed, keeping discharge away from the cutting zone and allowing the next bar to be prepared during cutting.
5. Cutting Performance
Rated capability with the 3,000 W source: carbon steel to 12 mm, stainless steel to 8 mm, aluminum and brass to 6 mm, copper to 4 mm. Representative cutting speeds:
| Material | Thickness (mm) | Cutting Speed (m/min) | Assist Gas |
|---|---|---|---|
| Carbon steel | 1 | 7–10 / 20–25 | Oxygen / air |
| Carbon steel | 2 | 5–7.5 / 13–17 | Oxygen / air |
| Carbon steel | 4 | 3.5–4.5 | Oxygen / air |
| Carbon steel | 8 | 1.6–2.3 | Oxygen / air |
| Carbon steel | 12 | 0.9–1.2 | Oxygen / air |
| Stainless steel | 1 | 20–25 | Nitrogen |
| Stainless steel | 2 | 12–15 | Nitrogen |
| Stainless steel | 4 | 3.5–4.5 | Nitrogen |
| Stainless steel | 6 | 1.3–1.8 | Nitrogen |
| Stainless steel | 8 | 0.8–1 | Nitrogen |
| Aluminum alloy | 1 | 20–25 | Nitrogen |
| Aluminum alloy | 2 | 13–17 | Nitrogen |
| Aluminum alloy | 4 | 3.5–4.5 | Nitrogen |
| Aluminum alloy | 6 | 1.3–1.8 | Nitrogen |
| Brass | 1 | 22–26 | Nitrogen |
| Brass | 2 | 10–15 | Nitrogen |
| Brass | 4 | 2.5–3.5 | Nitrogen |
| Brass | 6 | 1–1.5 | Nitrogen |
| Copper | 1 | 20–25 | Oxygen |
| Copper | 2 | 9–12 | Oxygen |
| Copper | 3 | 3.5–5.5 | Oxygen |
| Copper | 4 | 2.2–2.5 | Oxygen |
6. Power, Cooling & Gas Requirements
| Item | Requirement |
|---|---|
| Power supply | Three-phase five-wire 380–400 VAC, 50 Hz; recommended capacity ≥ 60 kVA, voltage stability ± 2%, grounding resistance ≤ 3 Ω |
| Cooling water | 40 L distilled / deionized water, conductivity < 10 µS/cm |
| Assist gas | Oxygen purity ≥ 99.6%; nitrogen purity ≥ 99.99% |