Product Parameters:
1. Machine Overview
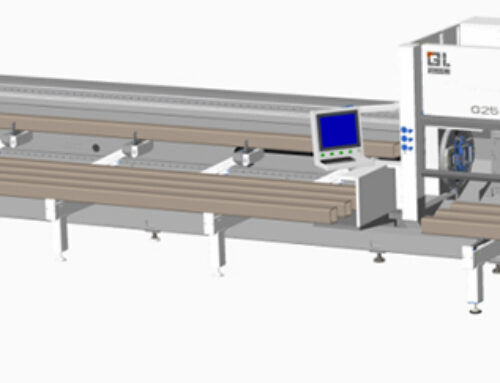
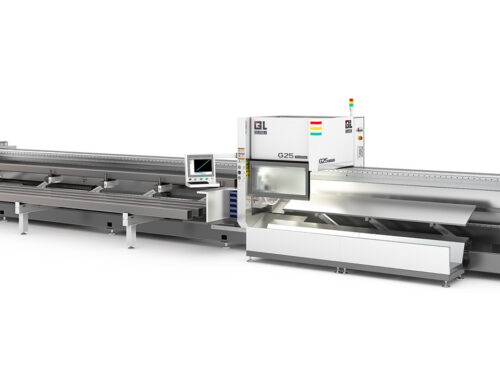
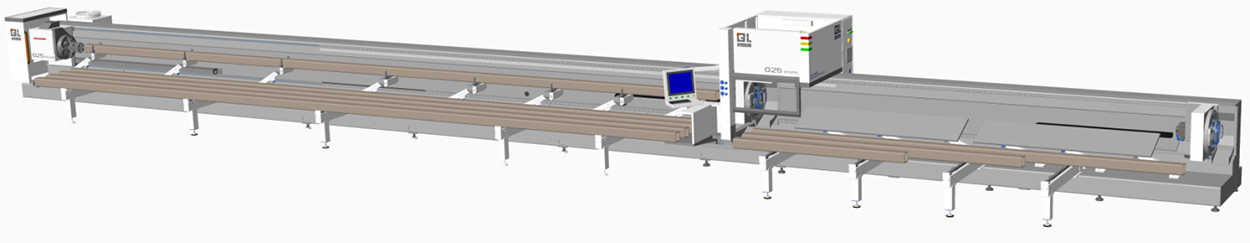
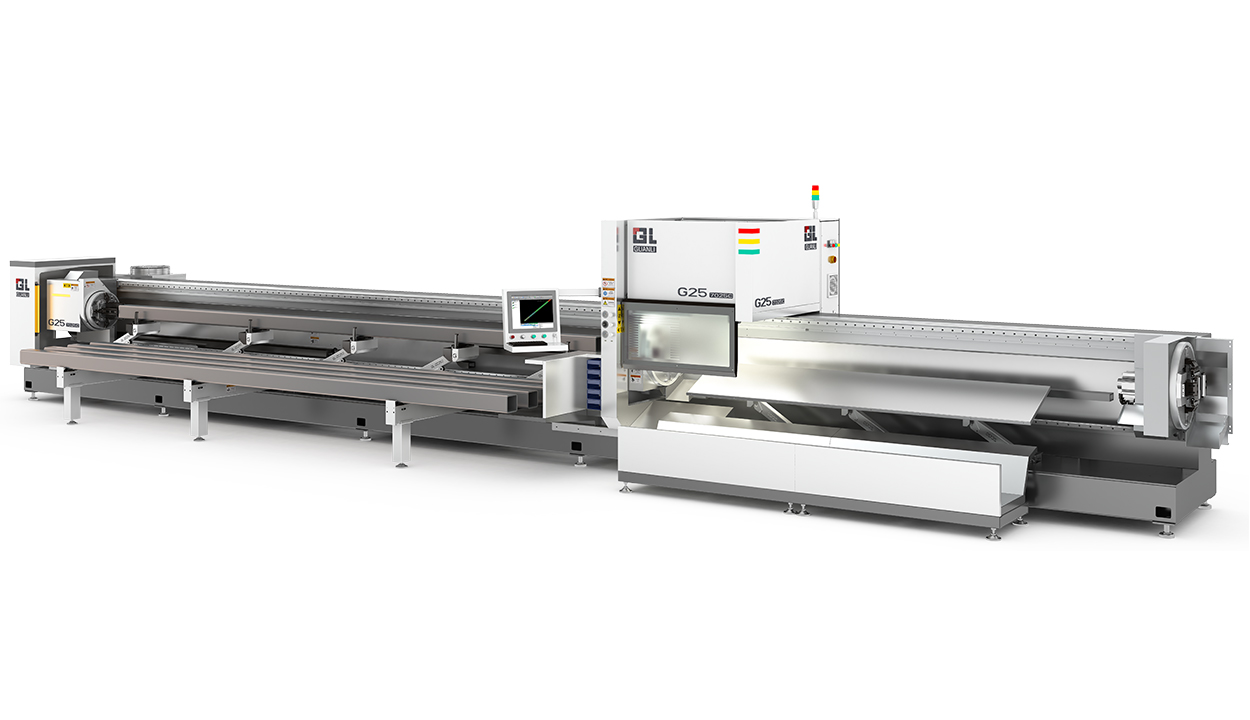
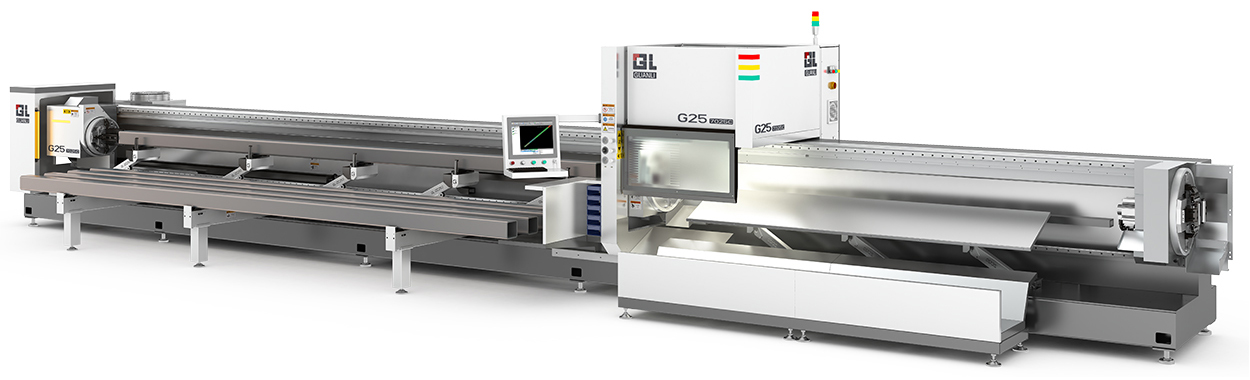
The GT25-7025Q-3000W combines a 3,000 W fiber laser with the GT25 chassis, which matches the G25B platform parameter set: side-suspended chuck structure, split welded bed (main cutting bed plus unloading bed), and clamping for round, square, oval and special-profile tubes from Φ15 mm to Φ250 mm. Tail waste is held to 20–45 mm, and running cost is approximately CNY 20–25 per hour — a practical package for job shops cutting mixed tube lots.
2. Key Advantages
- 120 RPM / 1.2 G rotary axis — quick rotation and reversal for tight profiles.
- Φ15–250 mm range — round, square, oval and special profiles on one machine.
- 20–22 s loading cycle — semi-automatic feeding integrated with the chassis.
- 20–45 mm short tails — measurable material savings on every bar.
- 600 °C / 4.5 h annealed split bed — welded, furnace-cooled, finish-machined.
- ≈ CNY 20–25/h running cost.
3. Welded Machine Bed & Structure
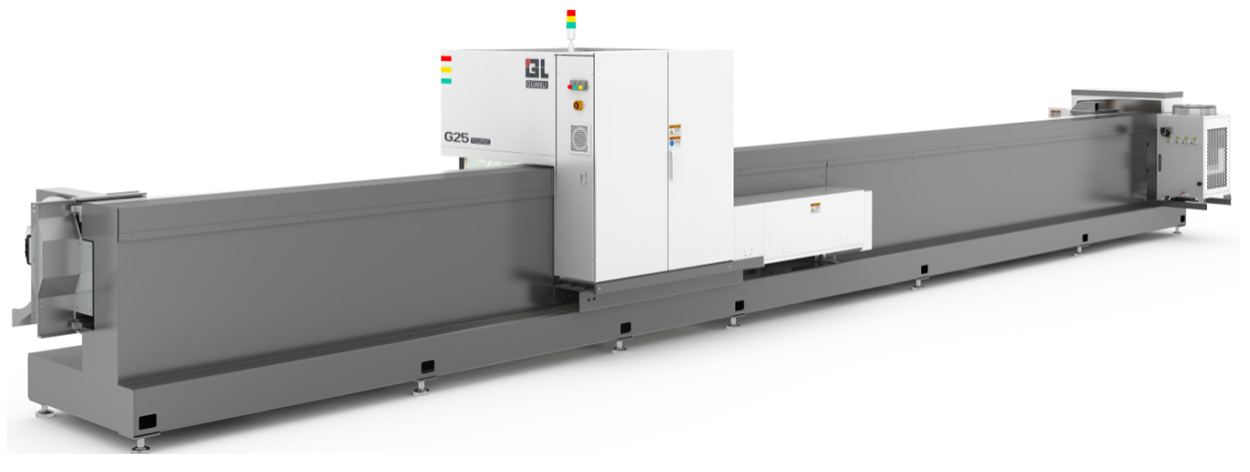
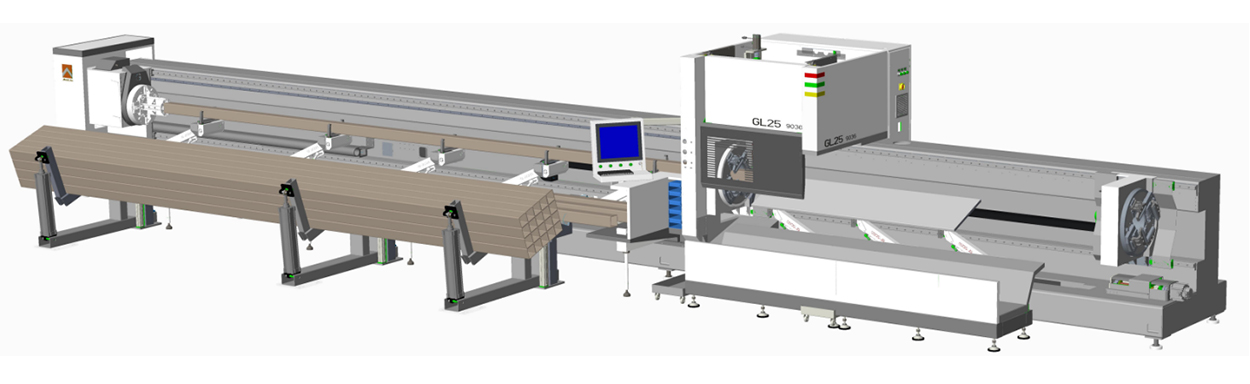
The GT25 bed is fabricated from welded steel plate and tube, annealed at 600 °C with a 4.5-hour hold and furnace cooling to relieve stress, then rough- and finish-machined. The split design pairs a main cutting bed with a separate unloading bed, while the side-suspended chuck leaves the tube line open for support and loading.
4. Automatic Loading System
A semi-automatic loading unit matched to the side-suspended structure loads each bar in 20–22 seconds. Cut parts are discharged onto the unloading bed, so the next bar can be staged while cutting continues.
5. Cutting Performance
The 3,000 W source handles carbon steel to 12 mm, stainless steel to 8 mm, aluminum and brass to 6 mm, and copper to 4 mm, with 0.1–0.8 s piercing on carbon steel. Representative cutting speeds:
| Material | Thickness (mm) | Cutting Speed (m/min) | Assist Gas |
|---|---|---|---|
| Carbon steel | 1 | 7–10 / 20–25 | Oxygen / air |
| Carbon steel | 2 | 5–7.5 / 13–17 | Oxygen / air |
| Carbon steel | 4 | 3.5–4.5 | Oxygen / air |
| Carbon steel | 8 | 1.6–2.3 | Oxygen / air |
| Carbon steel | 12 | 0.9–1.2 | Oxygen / air |
| Stainless steel | 1 | 20–25 | Nitrogen |
| Stainless steel | 2 | 12–15 | Nitrogen |
| Stainless steel | 4 | 3.5–4.5 | Nitrogen |
| Stainless steel | 6 | 1.3–1.8 | Nitrogen |
| Stainless steel | 8 | 0.8–1 | Nitrogen |
| Aluminum alloy | 1 | 20–25 | Nitrogen |
| Aluminum alloy | 2 | 13–17 | Nitrogen |
| Aluminum alloy | 4 | 3.5–4.5 | Nitrogen |
| Aluminum alloy | 6 | 1.3–1.8 | Nitrogen |
| Brass | 1 | 22–26 | Nitrogen |
| Brass | 2 | 10–15 | Nitrogen |
| Brass | 4 | 2.5–3.5 | Nitrogen |
| Brass | 6 | 1–1.5 | Nitrogen |
| Copper | 1 | 20–25 | Oxygen |
| Copper | 2 | 9–12 | Oxygen |
| Copper | 3 | 3.5–5.5 | Oxygen |
| Copper | 4 | 2.2–2.5 | Oxygen |
6. Power, Cooling & Gas Requirements
| Item | Requirement |
|---|---|
| Power supply | Three-phase five-wire 380–400 VAC, 50 Hz; recommended capacity ≥ 60 kVA, voltage stability ± 2%, grounding resistance ≤ 3 Ω |
| Cooling water | 40 L distilled / deionized water, conductivity < 10 µS/cm |
| Assist gas | Oxygen purity ≥ 99.6%; nitrogen purity ≥ 99.99% |